logo
Supal (Changzhou) Precision Tools Co.,Ltd
Sobre nosotros
Su socio profesional y confiable.
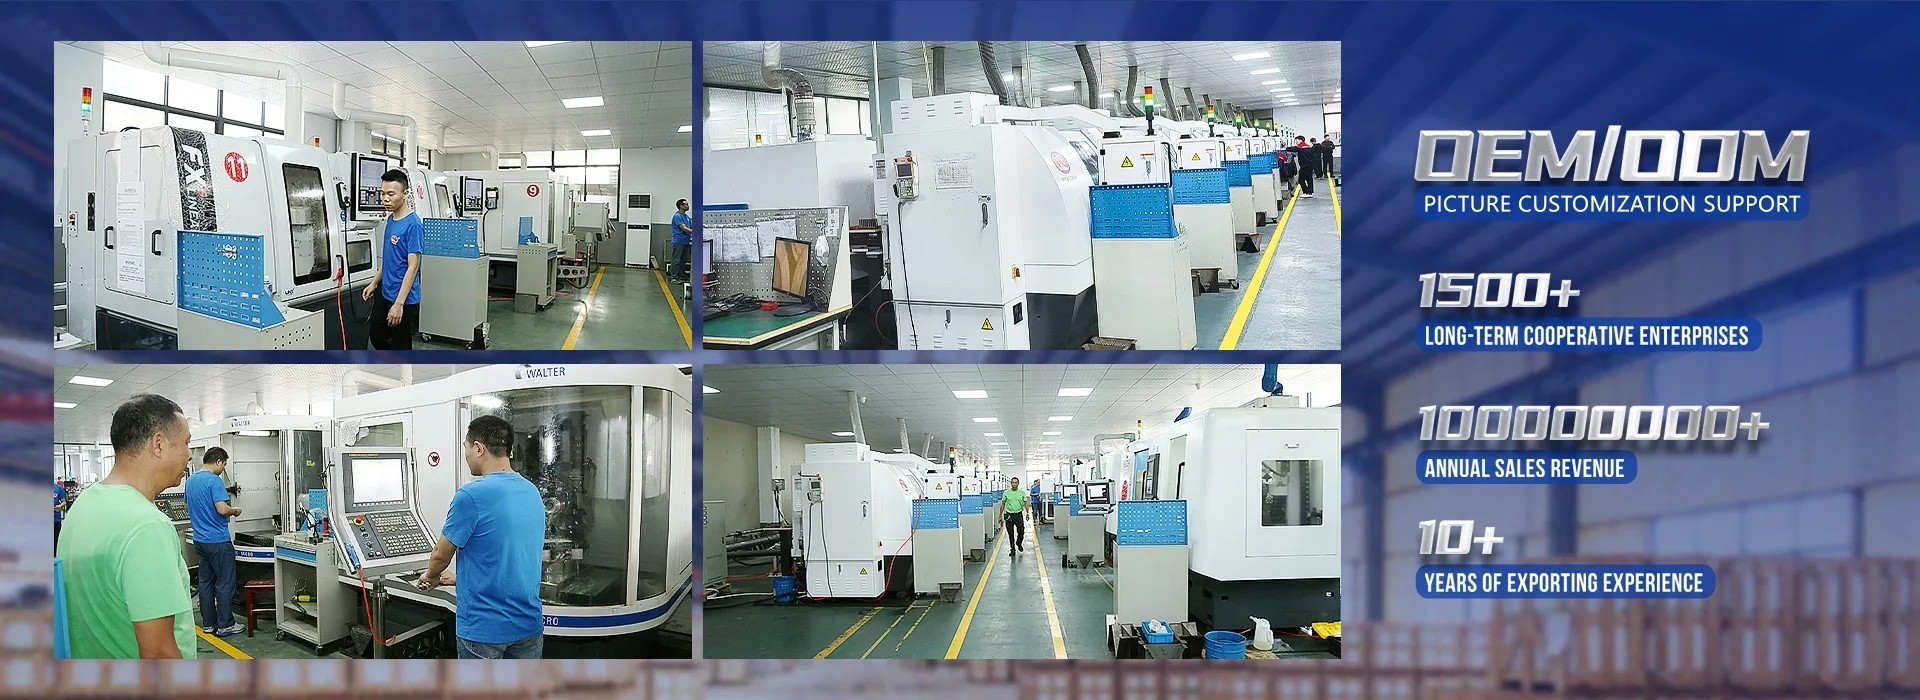
Supal (Changzhou) Precisión Herramientas Co., Ltd.Desde hace muchos años se dedica al diseño, producción y comercialización de herramientas de carburo sólido,con una inversión total de más de 10 millones, y está compuesta por un grupo de empleados experimentados.Como fabricante profesional de herramientas, se ha convertido en uno de los miembros directores de la Asociación de Herramientas de Changzhou Xiaxiashu.ANCA de Australia y máquinas de rectificación de cortadores NC de cinco ejesAdemás, ...
Aprenda más

0

Año establecido:

0

Millón+
Empleados

0

Millón+
Ventas anuales:
CHINA Supal (Changzhou) Precision Tools Co.,Ltd Alta calidad
Sello de confianza, verificación de crédito, RoSH y evaluación de la capacidad del proveedor. La empresa tiene un estricto sistema de control de calidad y un laboratorio de pruebas profesional.
CHINA Supal (Changzhou) Precision Tools Co.,Ltd Desarrollo
Equipo interno de diseño profesional y taller de maquinaria avanzada. Podemos cooperar para desarrollar los productos que necesita.
CHINA Supal (Changzhou) Precision Tools Co.,Ltd Producción
Máquinas automáticas avanzadas, estrictamente sistema de control del proceso. Podemos fabricar todos los terminales eléctricos más allá de su demanda.
CHINA Supal (Changzhou) Precision Tools Co.,Ltd 100% de servicio
Envases a granel y pequeños envases personalizados, FOB, CIF, DDU y DDP. Permítanos ayudarle a encontrar la mejor solución para todas sus preocupaciones.

Calidad Herramientas de fresado de carburo & Molinos de extremos cuadrados Fabricante

Encuentre los productos que mejoran para cumplir sus requisitos.
Casos y noticias
Los últimos puntos calientes.
Corner Radius vs Square End Mills for Interrupted Shoulder Milling
Corner Radius vs Square End Mills for Interrupted Shoulder Milling Interrupted shoulder milling is one of the operations where end mill geometry has a direct effect on edge stability. When the cutter repeatedly enters and exits the workpiece, passes across gaps, or encounters uneven stock, each tooth experiences a changing load instead of a smooth continuous cut. A square end mill can produce a sharp 90-degree shoulder, while a corner radius end mill can distribute load around the tool corner and reduce local stress. Choosing between them requires more than looking at the drawing requirement. For CNC machinists, process engineers, and purchasing engineers, the correct decision depends on the balance between required corner definition, interruption severity, tool rigidity, material, engagement, and finishing strategy. This guide compares square and corner-radius geometries for interrupted shoulder milling and explains how to diagnose edge chipping, chatter, poor finish, and unstable tool life. What Makes Interrupted Shoulder Milling Difficult? In a continuous side-milling cut, the cutting edge enters the workpiece and remains engaged in a relatively predictable way. In an interrupted shoulder operation, the edge may encounter a slot, a cross-hole, a casting irregularity, a forged surface, a previous pocket, or an open boundary. Each interruption changes the force and can create impact at entry or exit. The highest-risk conditions usually include: Repeated entry and exit at the same corner of the tool Full radial engagement at a 90-degree shoulder Thin walls or weak workholding that move during the cut Long tool overhang or poor holder runout Abrasive scale, cast skin, or hard inclusions Excessive feed or engagement at the interruption point A sharp square corner exposed to repeated impact A tool can therefore fail even when the average cutting load appears acceptable. The peak impact load, not only the average spindle load, may determine whether the edge survives. Square End Mills: Strengths and Limits A Square End Mill is the natural choice when the part requires a sharp internal shoulder or a flat-bottomed slot. Its geometry can produce a defined 90-degree corner without leaving a programmed radius at the bottom of the wall. When a Square End Mill Is Appropriate Square end mills are often considered when: The finished feature requires a sharp shoulder The toolpath uses stable, continuous engagement The workpiece and fixture are rigid The interruption is limited or can be approached with a controlled entry A separate finishing pass can protect the final corner quality The tool diameter and reach provide sufficient core strength A square tool can perform well in interrupted milling when the edge is properly supported and the engagement is controlled. It should not be rejected simply because the cut is interrupted; the severity and location of the interruption matter. Where Square Corners Become Vulnerable The tool corner is a stress concentration. During an interrupted cut, the corner may take a sudden impact as it enters the material. If the tool is also deflecting, the corner can receive more load than the other flutes. Typical results include corner chipping, a small radius appearing on the part after wear, chatter marks, or an abrupt change in surface finish. A sharp corner can also be sensitive to hard spots, scale, and thin-wall movement. If the failure is concentrated at the corner while the side cutting edges remain relatively intact, geometry and engagement should be reviewed before changing coating alone. Corner Radius End Mills: Strengths and Limits A Corner Radius End Mill includes a controlled radius between the end face and peripheral cutting edge. The radius removes the most fragile sharp corner and distributes cutting load over a larger region of the tool tip. When a Corner Radius Is Advantageous A corner-radius tool is often considered when: The cut includes repeated entry and exit The operation encounters an interrupted or uneven surface Edge chipping is concentrated at a square corner The part drawing permits a small internal radius The operation uses higher engagement or heavier roughing The process needs additional corner strength and more stable tool life The radius does not eliminate vibration or poor setup conditions, but it can reduce the severity of a localized corner impact. It may also improve the tool’s tolerance of intermittent engagement when compared with an otherwise similar sharp-corner tool. The Geometric Trade-Off The main limitation is straightforward: a corner radius leaves a radius on the finished shoulder. If the part requires a sharp 90-degree internal corner, the radius may need to be removed by a secondary operation or replaced by a square finishing tool. A corner radius can also change the effective engagement and contact area. It should be evaluated together with axial depth, radial engagement, tool diameter, and the required surface finish rather than selected based on radius size alone. How to Choose Between the Two Geometries Start With the Drawing Requirement First identify whether a sharp internal corner is functionally required or simply shown as a nominal feature. If a small radius is acceptable, a corner-radius tool may provide a more robust roughing or semi-finishing process. If a sharp corner is essential, use a square tool where practical or plan a roughing-and-finishing sequence that controls the load on the final square edge. Identify the Interruption Type Not all interruptions have the same effect. A predictable open boundary may be easier to manage than a hard casting skin or an irregular forged surface. Cross-holes and slots can create repeated impact at a known location, while uneven stock can make the load unpredictable. Record where the first damage occurs. If chipping starts at every entry point, the issue may be impact or lead-in strategy. If it appears only at a particular section of the workpiece, inspect material condition and support at that location. Match the Tool to the Operation For roughing and semi-finishing, the added corner support of a radius can be valuable when the operation is interrupted. For finishing, a square tool may be preferred if the corner specification requires it and the setup can maintain stable engagement. A practical process may use a corner-radius tool for stock removal, followed by a square end mill for the final shoulder. The two tools should not automatically use identical cutting conditions; the finishing tool may require a different engagement and a more controlled pass. Geometry, Edge Preparation, and Coating Edge Preparation A completely sharp edge may reduce cutting force in some materials, but it can be vulnerable to impact. A lightly reinforced edge may provide better stability in interrupted cuts, although excessive edge honing can increase rubbing and heat. The appropriate edge preparation depends on the workpiece, interruption severity, tool diameter, and operation. When comparing tools, request information about edge preparation rather than evaluating only flute count or coating name. Two tools with similar descriptions may behave differently if their edge preparation and carbide substrate differ. Helix and Flute Configuration Helix and flute count influence force direction, chip evacuation, and the number of teeth sharing the load. A higher flute count may support feed capacity in a light radial finishing pass, while a roughing or interrupted operation may need more chip space and a stronger core. The right balance depends on the material and engagement. A tool with insufficient flute space may recut chips, while a tool with a very thin core may lack impact resistance. Select from the broader Carbide Milling Tools range based on the actual operation rather than relying on the end mill shape alone. Coating Coating should follow the dominant failure mechanism. A coating may help manage heat, adhesion, or abrasive wear, but it cannot compensate for excessive tool deflection, a sharp corner overloaded by impact, or an unstable fixture. If the tool chips at entry, check geometry and rigidity before assuming that a coating change is the primary solution. Any coating recommendation should be validated with the specific material, tool geometry, coolant strategy, and cutting conditions. Treat supplier data as a starting reference and confirm the result on the actual machine. Parameter Strategy for Interrupted Shoulder Milling Cutting data should be treated as a starting reference for the exact diameter, flute count, coating, material grade, tool overhang, and machine setup. Do not transfer a value from a continuous side-milling operation directly to an interrupted shoulder cut without validation. Control the Peak Load at Entry Entry conditions can create the highest impact. Where the geometry allows, use a ramp, arc, or controlled lead-in instead of an abrupt radial plunge. This reduces the sudden change from no load to full engagement. If a direct entry is unavoidable, review feed and radial engagement at the entry point. A controlled reduction in engagement or a separate approach pass may protect the edge better than reducing the entire program feed. Avoid Excessive Full-Width Engagement Full-width shoulder milling creates significant radial load. In an interrupted condition, the load can change sharply as the tool crosses the gap. If possible, use a reduced radial engagement strategy for roughing and leave a controlled allowance for finishing. The correct engagement depends on the tool, material, machine, and feature geometry. Validate changes with spindle load, sound, chip form, and edge inspection rather than assuming that a smaller engagement is always better. Adjust Speed and Feed One Variable at a Time If the tool chips, do not immediately reduce both speed and feed. First determine whether the damage is impact-related, vibration-related, or caused by rubbing. A feed reduction that is too large can create a thin chip and increase rubbing, while a speed change may affect heat and resonance differently. Change one parameter at a time and document the effect. Include the location of the failure, chip appearance, surface finish, and tool condition in the record. Diagnosing Common Failure Symptoms Corner Chipping on a Square End Mill Check interruption severity, tool entry, runout, edge preparation, and whether the square corner is taking the full impact. If the drawing permits it, compare a corner-radius tool in the roughing or semi-finishing stage. If a square corner is mandatory, reduce entry shock and ensure the finishing pass has consistent stock. Chatter on a Corner-Radius Tool A radius does not remove the need for rigidity. Check tool overhang, holder condition, workholding, spindle speed, axial depth, and radial engagement. Chatter may also result from a radius that creates an engagement pattern unsuitable for the current toolpath. Uneven Wear Between Flutes Uneven wear commonly points to runout, unequal flute loading, poor holder seating, or a workpiece that is moving. Inspect the shank, collet, holder, and setup before changing the tool geometry. Poor Shoulder Finish After Roughing A roughing tool with a damaged corner or built-up edge should not be used for a critical finishing pass. Clean the feature, use a sound finishing tool, and verify that the remaining allowance is consistent. If the finish still varies, inspect vibration and workholding. Short Tool Life at a Hard Spot If damage occurs only at a particular location, investigate material condition, scale, interrupted geometry, or inadequate support. A different corner geometry may help, but the toolpath and entry strategy should also be reviewed. Common Mistakes to Avoid Choosing a Square Tool Only Because the Part Has a 90-Degree Corner A square finishing tool may be correct for the final feature but unnecessarily vulnerable during heavy interrupted roughing. Separate stock removal from final corner generation when the process requires both robustness and a sharp corner. Assuming a Corner Radius Always Solves Chipping The radius can improve corner strength, but it does not fix excessive overhang, runout, unstable workholding, poor parameters, or a damaged holder. Reducing Feed Aggressively After Chipping A large feed reduction can cause rubbing and heat. Determine whether the first damage occurred at entry, during an interruption, or under continuous cutting before making broad changes. Ignoring Toolholding The geometry selected on paper cannot compensate for poor holder cleanliness, excessive runout, or unnecessary projection. Check the actual holder and machine setup. Mixing Roughing and Finishing Requirements One tool rarely provides the best combination of high interruption tolerance, high stock-removal capacity, sharp 90-degree finishing, and final surface quality. Define which pass is responsible for each requirement. FAQ Is a corner radius end mill stronger than a square end mill? The radius removes the sharpest corner stress concentration and can improve resistance to local chipping in some interrupted operations. The actual result still depends on material, edge preparation, tool diameter, engagement, rigidity, and parameters. Should I use a corner radius for every interrupted shoulder cut? No. If a sharp 90-degree corner is required, a square end mill may still be necessary for finishing. A corner-radius tool can be considered for roughing or semi-finishing when the part permits a radius or a secondary finishing operation. Why does my square end mill chip only at the entry point? The entry may create an impact or engagement spike. Check lead-in strategy, radial engagement, feed at entry, runout, workpiece support, and the condition of the material surface at the entry location. Can changing the coating stop corner chipping? Only when the dominant failure involves heat, adhesion, or wear that the new coating is suited to control. Coating cannot correct an overloaded corner, poor rigidity, abrupt entry, or excessive engagement. What information should I provide when requesting an end mill recommendation? Provide the material grade, shoulder and interruption geometry, required corner condition, tool diameter and reach, machine and holder details, current parameters, coolant method, tool wear pattern, and photographs of the damaged edge or finished shoulder. Conclusion The choice between a corner-radius and square end mill for interrupted shoulder milling should begin with the part requirement, then consider interruption severity, edge strength, tool rigidity, engagement, and finishing strategy. A square end mill provides a sharp corner but concentrates stress at the tool tip. A corner-radius end mill distributes load more gradually and may reduce local chipping when a radius is acceptable. For demanding operations, a two-stage process can balance both objectives: use a robust geometry for interrupted roughing or semi-finishing, then use a square tool for the final shoulder when the drawing requires a sharp corner. Build parameters from the supplier’s starting range, change one variable at a time, and validate the complete process on the actual machine and workholding. If your shoulder milling process shows corner chipping, chatter, poor finish, or inconsistent tool life, Contact Supal with the material grade, interruption geometry, current tool, tool overhang, parameters, and photos of the failure. This information helps identify a practical geometry and process starting point for on-machine validation.

2026

10/06

How to Choose Carbide End Mills for Copper and Brass Machining
How to Choose Carbide End Mills for Copper and Brass Machining Copper, brass, bronze, and other copper alloys are often described as easy-to-cut materials because they are softer than hardened steel. That description can be misleading. Copper alloys can create very different machining problems depending on their purity, temper, alloying elements, work-hardening behavior, and chip form. A tool that produces a clean result in free-machining brass may rub, smear, or generate built-up edge in a more adhesive copper grade. For CNC machinists, process engineers, and purchasing engineers, reliable copper alloy milling starts with matching the tool to the actual failure mechanism. Edge sharpness, flute space, chip evacuation, workholding, coolant, and parameter validation usually matter more than simply choosing the hardest or most expensive coating. This guide explains how to select carbide end mills for copper and brass machining while reducing adhesion, burrs, heat, and unstable tool life. Why Copper and Brass Need Material-Specific Tool Selection Copper alloys combine several characteristics that influence milling stability: Copper conducts heat efficiently, so heat can move into the workpiece instead of remaining concentrated at the tool edge. However, local rubbing can still raise edge temperature and cause adhesion. Pure or highly ductile copper can produce continuous, gummy chips that are difficult to evacuate. Brass and bronze grades vary widely. Some produce short chips, while others create longer chips or abrasive particles. A dull edge may rub and smear the surface rather than shear it cleanly. Thin walls, small features, and poor workholding can amplify deflection and burr formation. The result is that “copper” or “brass” is not enough information for final tool selection. The exact alloy or grade, hardness or temper condition, feature geometry, and finishing requirement should be confirmed before adopting a production tool. Common Failure Symptoms in Copper Alloy Milling Built-Up Edge and Material Adhesion Built-up edge appears when copper or another ductile alloy adheres to the cutting edge. The tool may look sharp at the beginning of the cut but gradually develops a welded mass that changes the effective edge geometry. This can cause poor surface finish, burrs, dimensional variation, and sudden edge damage when the built-up material breaks away. Adhesion is often promoted by rubbing, insufficient chip evacuation, a dull edge, excessive dwell, or a surface treatment that is not suited to the material. Changing to a harder coating without correcting rubbing may not solve the problem. Smearing and Poor Surface Finish A smeared surface usually indicates that the tool is not shearing the material cleanly. Possible causes include insufficient chip thickness, a dull or heavily honed edge, poor tool runout, unstable workholding, or a speed/feed combination that leaves the tool rubbing instead of cutting. Burrs at Entry and Exit Copper and brass can produce burrs when the cutting edge pushes material away at the exit. Burr formation is influenced by tool sharpness, radial engagement, feed direction, workpiece support, and the condition of the edge. A finishing pass may reduce burrs, but the root cause should still be addressed in the toolpath and tool selection. Chipped Edge or Unexpected Tool Failure Carbide edge chipping in copper alloy milling is not always caused by a material that is too hard. Interrupted cuts, loose workholding, excessive runout, thin-wall deflection, collisions, and trapped chips can generate impact loads that damage the edge. If chipping is concentrated on one flute, inspect runout and setup balance before changing the carbide grade. Chip Packing and Recutting Long copper chips can remain in a pocket, slot, or narrow cavity. Once recut, they create additional heat and load, increasing the chance of built-up edge and surface scratching. Tool geometry and air or coolant direction should be selected with chip travel in mind, especially in deep features. Flute Geometry and Edge Sharpness Choose Enough Chip Space for the Operation Copper and ductile brass grades may require generous flute space so chips can leave the cutting zone before they are recut. A low-flute-count tool can be useful when chip evacuation is the primary limitation, but the correct flute count also depends on rigidity, engagement, feed, finish, and feature geometry. For a deep pocket or slot, prioritize a toolpath and geometry that provide a clear chip path. For a light finishing pass, a different flute configuration may be preferred if it provides the required surface quality without creating excess rubbing. Favor a Clean, Sharp Cutting Edge A sharp edge generally helps shear copper and brass rather than push or smear them. Excessive edge rounding can increase rubbing and heat. However, sharpness must be balanced against the risk of edge damage in interrupted cuts, cast surfaces, abrasive inclusions, or unstable fixtures. The best edge preparation is application-dependent. A stable finishing cut may benefit from a very sharp edge, while a roughing operation with impact risk may require controlled edge reinforcement. Request the intended edge preparation when comparing tools rather than judging only by the product title. Consider Polished Flutes and Rake Surfaces A smooth flute and rake surface can reduce friction and help chips slide away from the cutting edge. This is particularly relevant when the material tends to adhere or when the tool is used in a narrow cavity with limited chip clearance. Polishing alone does not replace the need for suitable flute volume, coolant, or air blast, but it can support cleaner chip transport. Coating and Substrate Considerations Copper alloy applications do not always benefit from the same coating choices used for hardened steel. The dominant issue may be adhesion and friction rather than oxidation or high-temperature wear. In some applications, uncoated polished carbide is appropriate because the sharp, low-friction surface is more important than a hard coating layer. For abrasive copper alloys, bronze grades, or materials containing hard particles, a coating or substrate selected for wear resistance may be useful. The correct choice depends on the exact alloy and failure mode. Do not assume that a coating marketed for hardened steel will automatically improve copper machining, and do not assume that an uncoated tool is correct for every bronze or filled alloy. When comparing copper tools with End Mills for Aluminum, use the aluminum tool as a reference only, not as an automatic substitute. Both material groups can be adhesion-prone, but the exact chip form, edge condition, and surface requirement may differ. Parameter Strategy for Copper and Brass Milling Start With the Actual Tool and Alloy Cutting data should be treated as a starting reference, not a guaranteed setting. The appropriate speed, feed, radial engagement, and axial depth depend on tool diameter, flute count, stickout, machine rigidity, workholding, alloy grade, and coolant or air-blast conditions. Validate the starting range on the actual machine before making it a standard process. Avoid Rubbing and Dwell If the tool spends too much time sliding along the surface, adhesion and smearing become more likely. Check whether the toolpath includes dwell at corners, excessive radial engagement, or a feed value that is too low for the selected edge geometry. A modest, controlled chip load is usually preferable to a cut dominated by rubbing, but the exact value must be validated for the tool and material. Control Chip Evacuation Direct air or coolant so chips move away from the cutting zone rather than being pushed back into the pocket. If chips are long, review flute volume, toolpath engagement, and the conditions that determine chip formation. Increasing fluid pressure without correcting nozzle direction or chip path may produce little improvement. Change One Variable at a Time When troubleshooting built-up edge, burrs, or poor finish, change only one major variable at a time: tool geometry, coating, speed, feed, engagement, or chip evacuation. Document the result. This makes it possible to identify the actual improvement instead of attributing every change to the last tool purchased. Toolholding, Workholding, and Feature Stability Even a well-selected tool can fail when the setup is unstable. Check tool runout, holder cleanliness, clamping length, and the shortest practical tool projection. Thin copper components and unsupported walls can deflect under cutting pressure, leaving burrs or dimensional error that look like a tool problem. For holes and finishing operations, coordinate the milling process with Carbide Drills and Carbide Reamers. A poor pre-hole or unstable entry can reduce the performance of the finishing tool even when the reamer itself is suitable. A Practical Selection and Troubleshooting Sequence Confirm the exact copper, brass, bronze, or copper-alloy grade and condition. Identify the dominant failure: adhesion, burrs, poor finish, chip packing, chipping, or dimensional drift. Select flute count and chip space based on engagement and chip travel, not on flute count alone. Review edge sharpness, rake surface, flute polish, coating, and substrate together. Check runout, overhang, workholding, and thin-wall support. Establish a conservative starting process and validate it on the actual setup. Adjust one variable at a time and record chip form, finish, burr condition, load behavior, and tool wear. Common Mistakes to Avoid Treating All Copper Alloys as Pure Copper Brass, bronze, and specialized copper alloys can produce very different chips and wear mechanisms. A recommendation for one grade should not be transferred automatically to another. Choosing Coating Before Identifying the Failure Mode If adhesion is the primary issue, friction and edge sharpness may deserve attention before thermal coating performance. If abrasion is dominant, the solution may require a different substrate or wear-resistant coating. Diagnose first. Using a Dull Tool for a Finishing Operation A worn edge can rub, smear, and create burrs even when the tool still appears usable. Replace or recondition the tool based on the required surface and dimensional result, not only on visible fracture. Ignoring Chip Travel in Pockets and Slots Long chips that remain in the cavity will be recut. Review toolpath direction, flute space, air blast, coolant placement, and the ability of the machine to clear chips. Copying Parameters From Steel or Aluminum Without Validation Copper alloy behavior is not identical to steel or aluminum. Use supplier data as a starting reference and confirm the process on the actual machine, workholding, and material grade. FAQ What type of carbide end mill is commonly used for copper? A sharp, low-friction tool with suitable chip space is often considered for copper, but the correct flute count, edge preparation, coating, and substrate depend on the exact alloy and operation. Confirm the choice against the material grade and feature geometry. Why does copper create built-up edge on the tool? Built-up edge is commonly associated with adhesion, rubbing, heat concentration, poor chip evacuation, or an edge condition that is not suited to the material. Review sharpness, flute polish, toolpath engagement, and validated parameters before changing coating alone. Is an uncoated carbide end mill suitable for brass and copper alloys? It can be suitable in some applications where a sharp, polished, low-friction edge is the priority. Abrasive bronze or filled copper alloys may require a different wear strategy. The exact recommendation should be confirmed for the specific grade and failure mode. How can I reduce burrs when milling copper? Check tool sharpness, runout, exit engagement, workpiece support, radial engagement, and feed direction. A finishing pass may help, but burr reduction is usually more reliable when the edge and toolpath are stable from the beginning. What information should I provide when requesting a copper alloy tool recommendation? Provide the exact alloy and condition, tool diameter and flute count, feature geometry, tool overhang, machine and holder details, current parameters, coolant or air-blast method, chip form, and photographs of the finish or worn edge. Conclusion Choosing carbide end mills for copper and brass machining requires more than selecting a standard tool for a soft material. The best starting point is to identify the alloy, failure mode, chip behavior, and setup stability. Sharp and suitable geometry, sufficient chip space, controlled friction, reliable evacuation, and validated parameters work together to reduce built-up edge, burrs, smearing, chipping, and inconsistent tool life. If your copper or brass operation has adhesion, burr, chip evacuation, surface-finish, or tool-life problems, Contact Supal with the material grade, feature geometry, current tool, parameters, and failure photos. This information helps evaluate a practical tool and process starting point for on-machine validation.
2026

10/01

Chatter y agujeros de gran tamaño: una guía para solucionar problemas
Rebabado de Carburo y Agujeros Sobredimensionados: Una Guía de Solución de Problemas El escariado a menudo se trata como una operación de acabado simple: taladre el agujero, pase el escariador y espere que el tamaño y el acabado de la superficie mejoren. En la práctica, el escariado con carburo es sensible a la holgura, la alineación, la rigidez, la entrega de refrigerante, la geometría del filo y la estabilidad de los parámetros. Cuando alguna de estas variables es incorrecta, el proceso puede producir marcas de rebabado, agujeros sobredimensionados, poca redondez, agujeros cónicos, mellas en el filo o una vida útil inesperadamente corta de la herramienta. Para los maquinistas CNC, ingenieros de procesos e ingenieros de compras, el punto clave es este: los escariadores no corrigen todos los problemas de taladrado. Un escariador puede mejorar un agujero preparado, pero no puede arreglar de manera confiable un pre-agujero severamente desalineado, rayado, subdimensionado, abocinado o inestable. Esta guía explica cómo diagnosticar el rebabado del escariador de carburo y los problemas de tolerancia del agujero paso a paso, para que la acción correctiva se base en el modo de falla en lugar de la suposición. ¿Por qué los problemas de escariado son difíciles de diagnosticar Un escariador de carburo corta con múltiples dientes a la vez y elimina solo una pequeña cantidad de material. Debido a que la operación es ligera en comparación con el taladrado o el fresado, muchos talleres asumen que el escariado debería ser indulgente. En realidad, la pequeña holgura de material y el objetivo de tolerancia ajustada hacen que el proceso sea menos indulgente. Si la holgura de escariado es demasiado pequeña, la herramienta puede rozar en lugar de cortar. Si la holgura es demasiado grande, los filos de corte pueden sobrecargarse. Si el agujero taladrado no está recto, el escariador puede seguir el error existente o verse forzado a cortar de manera desigual. Si el portaherramientas o el accesorio carecen de rigidez, una pequeña vibración puede aparecer como líneas de rebabado visibles dentro del agujero. Es por eso que el mismo escariador puede producir un excelente acabado en una configuración y fallar en otra configuración con el mismo diámetro nominal de agujero. Síntomas comunes en el escariado con carburo Marcas de rebabado dentro del agujero Las marcas de rebabado generalmente aparecen como patrones repetidos en espiral o poligonales en la pared del agujero. Indican que la herramienta, el portaherramientas, la pieza de trabajo o la estructura de la máquina están vibrando durante el corte. El rebabado puede ser causado por una holgura excesiva, rigidez insuficiente, mala alineación, velocidad incorrecta o un pre-agujero inestable. Agujeros sobredimensionados después del escariado Un agujero sobredimensionado puede ser causado por descentramiento de la herramienta, desalineación, presión de corte excesiva, expansión térmica o virutas atrapadas entre el escariador y la pared del agujero. Si los agujeros sobredimensionados se repiten consistentemente, mida el descentramiento y verifique la condición del pre-agujero antes de asumir que el diámetro del escariador es incorrecto. Acabado superficial deficiente Un acabado superficial deficiente después del escariado puede provenir de un filo construido, refrigerante inadecuado, re-corte de virutas, mala preparación del taladro o un filo desgastado. Cuando un escariador se ve obligado a eliminar material desigual, el acabado superficial a menudo empeora, incluso si la herramienta está afilada. Vida útil corta o inconsistente de la herramienta Si un escariador dura mucho más que otro en la misma aplicación, revise la configuración de la máquina, la preparación del agujero, la entrega de refrigerante y la variación del material de la pieza. El recubrimiento de la herramienta y el grado de carburo importan, pero la inestabilidad del proceso es a menudo lo primero que se debe eliminar. Mellas en el filo Las mellas en el filo de un escariador de carburo a menudo indican impacto, corte interrumpido, holgura excesiva, mala entrada o inclusiones duras en la pieza de trabajo. Los escariadores son herramientas de acabado; no están diseñados para corregir grandes errores de taladrado o eliminar material pesado. Causa raíz 1: Holgura de escariado incorrecta La holgura del pre-agujero es una de las variables más importantes en el escariado. Muy poco material puede causar rozamiento, calor y un acabado deficiente. Demasiado material puede sobrecargar el filo de corte y causar rebabado o mellas. No existe una holgura universal que se adapte a cada diámetro, material y diseño de escariador. Como principio inicial, los agujeros de diámetro pequeño generalmente necesitan holguras más pequeñas, mientras que los agujeros más grandes pueden tolerar una mayor eliminación de material. Sin embargo, el valor correcto depende del material de la pieza de trabajo, la profundidad del agujero, la geometría de la herramienta, el método de refrigeración y el objetivo de tolerancia. Siempre valide la holgura en la máquina y el accesorio reales en lugar de copiar un valor de otra operación. Al solucionar problemas, compare el diámetro real del agujero taladrado antes del escariado con el objetivo final. Si el tamaño del pre-agujero varía de una pieza a otra, el resultado del escariado también variará. Causa raíz 2: Mala calidad del pre-agujero Un escariador necesita una guía estable. Si el agujero taladrado ya está fuera de posición, cónico, rayado o endurecido por trabajo, el escariado se vuelve mucho más difícil. Antes de culpar al escariador, inspeccione el proceso de taladrado. Verifique si el taladro produce un agujero redondo y recto, si las virutas están rayando la pared y si el taladro se desvía en la entrada. Para el control del proceso de creación de agujeros, Taladros de Carburo y los escariadores deben seleccionarse como un sistema, no como herramientas no relacionadas. Si el taladro deja rayaduras severas de virutas o un tamaño de agujero inconsistente, el escariador puede no tener suficiente control para reparar el defecto. Mejore la estabilidad del taladrado primero, luego evalúe el paso de escariado. Causa raíz 3: Descentramiento y desalineación El descentramiento es una de las formas más rápidas de producir agujeros sobredimensionados y desgaste desigual de la herramienta. Una pequeña cantidad de descentramiento en el portaherramientas o el husillo puede hacer que un filo de corte haga más trabajo que los otros. Esto crea una presión de corte desigual, una redondez deficiente y una vida útil más corta de la herramienta. Verifique el descentramiento en el vástago de la herramienta y cerca de la sección de corte cuando sea posible. También revise la condición del portaherramientas, la limpieza de la pinza, la condición del husillo y si la herramienta está sujeta con suficiente longitud de contacto. Para agujeros de precisión, el sistema de sujeción de la herramienta es tan importante como el escariador mismo. La desalineación también puede ocurrir cuando el escariador entra en un agujero que no es coaxial con la trayectoria del husillo. Esto es común cuando operaciones previas, accesorios o configuraciones de largo alcance introducen deflexión. Causa raíz 4: Velocidad, avance y estabilidad de corte Los parámetros de escariado deben ser lo suficientemente estables como para cortar limpiamente sin rozamiento ni vibración. Una velocidad demasiado alta puede aumentar el calor y empeorar el rebabado en algunos materiales. Un avance demasiado bajo puede causar rozamiento en lugar de corte. Un avance demasiado alto puede sobrecargar el filo y dañar el acabado superficial. Para solucionar problemas, ajuste una variable a la vez. Si aparece rebabado, reducir ligeramente la velocidad puede ayudar, pero solo si la rigidez y la holgura ya son razonables. Si la herramienta roza y produce calor, aumentar el avance dentro de un rango seguro a veces puede mejorar la acción de corte. Los cambios de parámetros deben verificarse mediante cortes de prueba en el material de la pieza real. Evite usar tablas genéricas de velocidad y avance como valores finales. Trátelos como referencias iniciales y ajústelos según el tamaño del agujero, la profundidad, la rigidez de la máquina, el refrigerante y los requisitos de tolerancia. Causa raíz 5: Control de refrigerante y virutas Aunque el escariado elimina menos material que el taladrado, las virutas siguen siendo importantes. Las virutas finas o partículas atrapadas dentro del agujero pueden rayar la pared y dañar los filos de corte. El refrigerante ayuda a evacuar las virutas, reducir el calor y estabilizar la zona de corte. Para agujeros ciegos, la evacuación de virutas se vuelve más difícil porque las virutas tienen espacio limitado para salir del fondo del agujero. La dirección, la presión y el flujo del refrigerante deben revisarse cuidadosamente. Si quedan virutas en el agujero del taladrado, limpie o enjuague el agujero antes de escariar. La concentración y filtración del refrigerante también importan. El refrigerante contaminado puede transportar partículas abrasivas de regreso al agujero, afectando el acabado superficial y la vida útil de la herramienta. Causa raíz 6: Geometría del escariador y ajuste de la aplicación Diferentes Escariadores de Carburo están diseñados para diferentes aplicaciones. Factores como el diseño de la ranura, el ángulo de ataque, el diseño del margen, la preparación del filo y el recubrimiento pueden influir en la estabilidad de corte y la evacuación de virutas. Un escariador para agujeros pasantes puede no comportarse de la misma manera en agujeros ciegos. Un escariador optimizado para aluminio puede no ser ideal para acero inoxidable o material endurecido. Un escariador largo puede requerir atención adicional a la rigidez y al descentramiento. Al discutir un problema de escariado con un proveedor, proporcione el material de la pieza de trabajo, el diámetro del pre-agujero, la tolerancia objetivo, la profundidad del agujero, la condición de agujero pasante o ciego, el método de refrigeración, los parámetros actuales y fotos de la superficie del agujero si están disponibles. Esta información ayuda a determinar si la solución es un cambio de geometría, un cambio de parámetros o una corrección del proceso. Un flujo de trabajo práctico de solución de problemas Paso 1: Medir el pre-agujero Antes de verificar el agujero terminado, mida el agujero taladrado o escariado antes de escariar. Registre el diámetro, la redondez, la rectitud si es posible y la condición de la superficie. Si el pre-agujero es inestable, arréglelo primero. Paso 2: Verificar el descentramiento de la herramienta Mida el descentramiento en el portaherramientas real. Limpie el vástago, la pinza y el portaherramientas. Reemplace los portaherramientas dañados o las pinzas desgastadas. Si el descentramiento se reduce y los agujeros sobredimensionados mejoran, el escariador no fue la causa principal. Paso 3: Revisar la holgura Compare el diámetro real del pre-agujero con el tamaño del escariador. Si la holgura varía entre piezas, identifique por qué la operación de taladrado o escariado es inconsistente. Paso 4: Inspeccionar virutas y acabado superficial Busque virutas atrapadas en el agujero, rayaduras o marcas de rozamiento. Si aparecen rayaduras de virutas, mejore la evacuación del refrigerante y la limpieza del pre-agujero. Paso 5: Ajustar parámetros gradualmente Cambie la velocidad, el avance o el refrigerante un factor a la vez. Registre los resultados. Evite cambiar la geometría de la herramienta y los parámetros simultáneamente a menos que la configuración actual sea claramente inadecuada. Paso 6: Revisar la selección de la herramienta Si el proceso es estable pero el problema persiste, revise la geometría del escariador, el recubrimiento, el estilo de la ranura y la preparación del filo. Para operaciones de mecanizado y acabado relacionadas, Supal también proporciona Herramientas de Fresado de Carburo para una planificación de procesos CNC más amplia. Errores comunes a evitar Error 1: Esperar que el escariador arregle un agujero defectuoso Un escariador es una herramienta de acabado, no una herramienta de rescate. Si el agujero taladrado está severamente descentrado, cónico o rayado, mejore el pre-agujero primero. Error 2: Ignorar el descentramiento El descentramiento puede hacer que un escariador preciso corte sobredimensionado. Siempre mida la herramienta en el portaherramientas real en lugar de asumir que la herramienta en sí es incorrecta. Error 3: Usar muy poca holgura Muy poco material puede causar rozamiento, calor y un acabado deficiente. La herramienta debe cortar, no pulir material irregular. Error 4: Usar demasiada holgura Demasiado material puede sobrecargar los filos de corte y causar rebabado, mellas o una redondez deficiente. Error 5: Cambiar el diámetro del escariador antes de verificar el proceso Si el agujero está sobredimensionado debido a descentramiento, desalineación o rebabado, cambiar el diámetro de la herramienta puede no resolver el problema raíz. Preguntas frecuentes ¿Por qué mi escariador de carburo produce un agujero sobredimensionado? Las causas comunes incluyen descentramiento, desalineación, holgura excesiva, calidad inestable del pre-agujero, virutas atrapadas o efectos térmicos. Mida el descentramiento y el tamaño del pre-agujero antes de asumir que el diámetro del escariador es incorrecto. ¿Puede un escariador corregir la desviación del taladro? Solo en grado limitado. Si el agujero taladrado está significativamente descentrado o no es recto, el escariador puede seguir el error existente. Mejore el proceso de taladrado o escariado primero. ¿Qué causa el rebabado durante el escariado? El rebabado puede resultar de una holgura excesiva, mala rigidez, velocidad incorrecta, voladizo largo de la herramienta, geometría inestable del pre-agujero o mala alineación entre el husillo y el agujero. ¿Debo reducir la velocidad o el avance para detener el rebabado del escariador? A veces, reducir la velocidad ayuda, pero no siempre es la primera solución. Verifique primero el descentramiento, la holgura, la rigidez del portaherramientas y la calidad del pre-agujero. Un avance demasiado bajo también puede causar rozamiento. ¿Qué información debo enviar al solicitar soporte para la solución de problemas de escariadores? Envíe el material de la pieza de trabajo, el diámetro del pre-agujero, el diámetro y la tolerancia objetivo, la profundidad del agujero, la condición de agujero pasante o ciego, el método de refrigeración, la velocidad/avance actual, el voladizo de la herramienta, el tipo de portaherramientas y fotos de la superficie del agujero o del escariador desgastado. Conclusión El rebabado del escariador de carburo, los agujeros sobredimensionados y la corta vida útil de la herramienta son generalmente problemas del proceso, no solo problemas de la herramienta. La secuencia de solución de problemas más efectiva es medir el pre-agujero, verificar el descentramiento, revisar la holgura, inspeccionar las marcas superficiales y ajustar los parámetros una variable a la vez. Si se enfrenta a tolerancias de agujero inestables, marcas de rebabado o una corta vida útil del escariador, Contacte a Supal con su material de pieza de trabajo, condición del pre-agujero, tolerancia objetivo, parámetros actuales y fotos de fallas. Supal puede ayudar a evaluar si la causa raíz es la holgura, el descentramiento, el refrigerante, la geometría del escariador o la estabilidad general del proceso.

2026

09/29